Third Generation Cement House Mold Buying Checklist for Smart Builders
2026-11-18
Most builders still choose cement house molds the way they did a decade ago—by price and a few photos. Third-generation molds have changed the math. Tolerances, vibration points, joint fit, and after-sales support now decide whether a mold pays for itself or becomes a yard problem. This checklist covers what smart builders actually inspect before committing. At LugongMachinery, we’ve watched too many projects stall over avoidable specs, so we kept this guide field-focused and fluff-free.
Frame Alignment Checks That Prevent Costly Panel Gaps Later
Getting the frame squared away before hanging sheet metal is one of those steps that feels slow in the moment and pays off every day after. A few millimeters of twist near the front rails can turn into a hood that sits proud on one side and a fender-to-door gap that widens at the bottom. Rather than chasing those mismatches with shims later, a careful check of the datum points—usually the factory locating holes and the upper torque boxes—gives you a much clearer picture of where the structure actually sits.
The checks that matter most are the ones done with the suspension loaded and the vehicle settled, not just sitting on jack stands at odd angles. Measure crosswise, front corner to opposite rear corner, and compare against the factory dimensions before assuming the rails are straight. Even a small sag at the cowl or a slight diamond condition will show up as uneven panel gaps once the doors and fenders go back on. Fixing that at the frame stage takes a fraction of the time it costs to realign sheet metal after paint.
It also helps to record the numbers before and after any pulling or welding. When the gaps come out even on the first test fit, that is usually the result of earlier checks catching the problem while it was still cheap to correct. If a panel still does not want to sit right, the frame measurements tell you whether to look at the panel itself or go back to the structure underneath.
Why Surface Finish Trials Beat Brochure Photos Every Time
A brochure photo shows you what a finish looked like on one good day, under one flattering light, after someone had time to clean it up. A trial panel shows you what actually arrives at your dock. Colors shift with angle, gloss levels change under factory lighting, and textures that look smooth in print can feel rough or waxy in your hand. If you can hold a sample, tilt it toward a window, run a fingernail across the edge, and compare it against the part it needs to match, you already know more than a staged image will ever tell you.
The differences get even more obvious on the edges and inside corners, where most finishes struggle. Photos rarely spend much time on those areas. A physical sample lets you check coverage around holes, along bends, and on the back side of a bracket, which is usually where adhesion and thickness fall apart. You can also keep that sample for a few weeks to see how it handles fingerprints, cleaning chemicals, or a humid afternoon. Brochures age well; real surfaces have to survive your environment.
There is also the matter of matching. Every monitor displays color differently, every print run drifts, and every camera adjusts white balance on its own. A trial finish gives you a stable reference you can put next to a powder-coated housing or an anodized extrusion and judge under the same light your team uses. That kind of comparison is far harder to argue with than a JPEG.
The Logistics Fine Print Builders Usually Discover Too Late
Most supplier quotes assume a best-case drop: a semi with a liftgate, a clear curb, and somebody on site ready to unload. What builders actually get is a driver who is contractually required only to leave the pallet at the curb. If the site lacks a telehandler or a loading dock at that exact moment, the crew ends up hauling framing lumber by hand from the street while the clock on the rental lift runs out.
The charges that sting rarely show up on the first page of the quote. Oversized trusses or long steel beams can trigger flatbed fees, overhang permits, and even escort vehicles for wide loads. Then there is detention: many carriers start billing after 15 or 30 minutes of waiting time, which turns a delayed concrete pour or a missed framing crew into a line item that arrives weeks later on the invoice.
Access restrictions are another slow-burn headache. A narrow cul-de-sac, low overhead wires, or a soft gravel entrance can force a transfer to a smaller shuttle truck, with the extra handling added to the final bill. Some builders also overlook storage clauses: if the site cannot accept a full truckload, the supplier may hold the material in a warehouse and charge daily storage, while early deliveries left outside become a magnet for weather damage and theft.
Mix Design Missteps That Manufacturers Use to Deny Warranty Claims
A warranty denial rarely hinges on a single catastrophic failure. More often, manufacturers comb through batch tickets and field logs looking for small deviations from the approved mix design. A water-cement ratio that drifts upward because a crew added water at the site, an admixture dosage changed without a revised submittal, or aggregates sourced from a different quarry can all become convenient justification. The language in the warranty typically requires strict conformity to the submitted recipe, not just a finished product that looks and performs acceptably.
Testing gaps hurt as much as the changes themselves. If the contractor cannot produce dated slump tests, moisture corrections, or calibration records for dispensers, the manufacturer may argue the placed concrete no longer matches the design that was originally approved. That argument works even when the real cause of a failure lies elsewhere, such as curing conditions or substrate preparation. Keeping the paper trail tied to the actual batching sequence, including any water added on site and any admixture adjustments, removes the easiest refusal path.
The practical fix is to treat every adjustment as a formal revision rather than a field convenience. If a pump requires more workability, request an updated mix design or have the producer's technical representative approve the change in writing before the pour continues. Otherwise, a defensive manufacturer can point to the altered mix as the reason for cracking, scaling, or delamination, even when the evidence is thin.
Third-Generation Features Worth the Extra Cost and Upgrade Claims Worth Ignoring
A third generation usually means the maker has had two rounds to learn what actually breaks, drains power, or annoys people. The upgrades that justify the higher price are rarely the ones featured on the box. Longer runtime under real load, quieter moving parts, tighter seals against dust and moisture, and sensors that stay accurate after months of use are the kind of fixes that separate a tool you live with from one you tolerate. Those improvements cost more because they require better components and tighter manufacturing, but they show up every day.
What you can safely tune out includes most cosmetic refreshes, a slightly rearranged app, and phrases like ‘new levels of comfort’ or ‘smarter performance’ when the core specifications have barely shifted. If a second-generation model still does its job and the advertised change is mainly visual or language-based, the extra spend is usually not paying for a meaningful difference. A new shade of finish or a redesigned button layout does not make the device more capable.
A useful test is to ask which exact task becomes faster, quieter, longer, or less annoying. If the answer is a measurable change, such as less weight, fewer charging cycles per week, or better cold-weather behavior, the premium may be worth it. If the answer is a vague feeling or an ‘upgraded experience,’ you are mostly paying for packaging. Third-generation products earn their price by removing known frustrations, not by renaming them.
How to Pressure-Test Spare Parts Support Before Your First Pour
Ask for a part that is slightly unusual but still something a serious supplier should keep in stock. A group gasket for an older revision, a bypass seal kit, or a specific O-ring set works well. Then ask for a photo of the actual shelf stock or the bin label. A supplier with real inventory rarely hesitates, because that photo takes ten seconds. A supplier who sends a brochure or a generic stock list is telling you something about how your future urgent order will go.
Give them a specific day and time when the machine must be running, and ask what the cutoff is for overnight shipping. You want to hear the hour, the carrier option, and the backup part number if the first choice is not available. If you get a vague answer about warehouses and typical lead times, treat it as a signal. That vagueness matters more before your first pour than after a breakdown.
Ask one compatibility question that only gets asked by people who maintain equipment. Does the current group gasket fit older portafilters? Does the pump kit include the small O-rings that usually need replacing? The answer should sound quick and slightly unremarkable, as if they have answered it many times before. If the reply is confused, slow, or deflected to another department, plan on storing a few critical spares yourself or choosing a different vendor.
FAQ
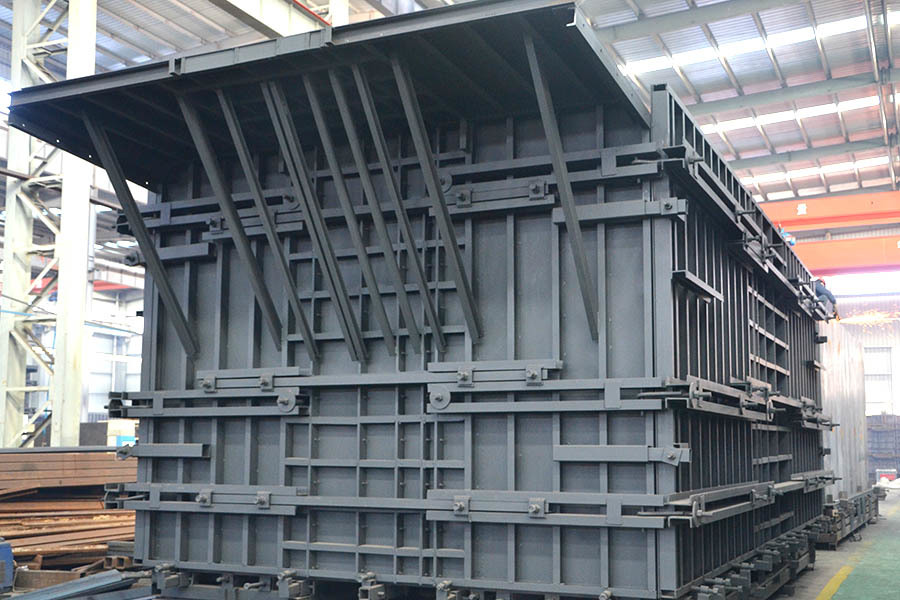
Start with the weld lines and corner joints. Look for full continuous beads, no undercut or porosity, and check whether the faceplate sits flat against the frame. If the diagonal measurements between opposite corners are off by more than a few millimeters, walk away.
A Q345 or equivalent structural steel frame with a 4mm to 6mm plate face tends to give the best balance between stiffness and easy stripping. Avoid thin sheeting that flexes under vibration, because that transfers straight into wall finish problems later.
Realistically, 300 to 500 pours if the crew cleans it after each cycle and keeps the contact surfaces oiled. The number drops fast when someone hammers hardened concrete off the face or skips the release agent because the site is behind schedule.
Ask for integrated window and door bucks, lifting anchors sized for the crane on site, and alignment guides on the corners. These are easier to add during fabrication than to rig up later with site-made brackets that never quite fit.
The hinge pins, locking clamps, and corner castings usually go first. Once those start to wear, the panels lose alignment and you get step lines on the wall surface. A low upfront price rarely covers the cost of reworking that kind of defect.
Request an actual tolerance report and then spot-check it yourself. Measure the diagonal across each panel, check the opening sizes for doors and windows, and run a straightedge along the faceplate. Do not accept a verbal promise that everything is within spec.
Remove concrete residue before it fully cures, use the release agent the manufacturer recommends, and store the panels off the ground with the faceplates protected from moisture. A few minutes of cleaning after each pour prevents most of the rust and buildup that shortens mold life.
That depends more on after-sale support than on the unit price. If an imported mold arrives with a damaged clamp or a warped panel, delays can eat the savings quickly. A local supplier with spare parts and a technician nearby is often the safer choice for builders running tight schedules.
Conclusion
Frame alignment is where most hidden costs start. Before signing anything, lay the mold sections on a level slab and run a straightedge across the joints, check diagonal measurements, and dry-assemble at least two corner panels. A small twist now becomes a panel gap you will fight on every pour. Surface finish should be judged from trial casts, not brochure shots. Bring your own aggregate, release agent, and mixing water, then cast a sample under site conditions. If the face shows pinholes, color drift, or sand streaks, that is the real finish. Logistics deserves the same scrutiny. Confirm the dismantled sections fit through gate openings and overhead clearances, know the lifting weight per piece, and check whether rust protection and transport insurance actually cover delivery to your site. Mix design records matter because manufacturers often deny warranty claims over minor water-cement ratio drift or unapproved admixtures. Keep dated batch logs, moisture readings, and mixing times from day one.
Third-generation upgrades are not all equal. Integrated vibration mounts, faster clamping systems, and replaceable liners earn their cost because they reduce labor and extend mold life. Claims like self-cleaning surfaces, zero maintenance, or universal mix compatibility usually fall apart in the field, so ask for a written performance example instead of a glossy spec sheet. Spare parts support should be tested before the first pour, not after a breakdown. Request a current inventory list of wear items such as seals, clamps, and corner brackets, ask for real lead times, and place a small paid order to see how the manufacturer handles dispatch, packaging, and tracking. Then remove and reinstall a few seals and bolts during inspection. If a supplier hesitates on any of these points, treat that as part of the mold's true price. Smart builders put alignment tolerances, trial cast acceptance, delivery terms, mix documentation duties, and spare parts response times into the purchase appendix and final acceptance sign-off.
Contact Us
Contact Person: Zhang Zhenlai
Email: [email protected]
Tel/WhatsApp: 8618563210000
Website: https://en.lugongmachinery.com/