Bespoke Rubber Tire Tread Cooling Production Line Tailored for Consistent Tread Quality
2026-11-17
Every tire tread carries the hidden signature of its cooling cycle. When temperatures drift, even slightly, tread quality becomes a gamble—something no tire manufacturer can afford. AUGU AUTOMATION approaches this challenge differently, building bespoke rubber tire tread cooling production lines around the exact output, layout, and consistency targets of each plant. This post looks at how tailored cooling engineering turns a demanding process into a repeatable advantage.
A Cooling Path Shaped by the Tread, Not a Standard Cycle
Most thermal designs assume the coolant should move in a predictable loop, entering one side and exiting the other with equal spacing. That assumption falls apart once the tread enters the picture. The contact patch creates uneven heat spikes, and the shoulders and center groove do not shed temperature at the same rate. So the path has to follow the tread blocks themselves, bending where they bend and slowing where the rubber holds more heat.
Instead of forcing a circular route, the channels are cut to mirror the actual load map. Under hard cornering, the outer blocks carry more stress, and the cooling path shifts its volume toward that area. The center rib may need only a narrow passage, while the intermediate grooves get wider channels because they sit right above the hottest part of the carcass. It is less like plumbing and more like tracing the footprint.
That irregular route also changes how pressure behaves. A standard cycle tends to equalize temperature gradually, but it often leaves isolated hot pockets between blocks. When the path is dictated by the tread geometry, those pockets are interrupted before they can build up. The result is a temperature spread that follows the tire's actual working shape rather than a clean but unrealistic loop.
Spray Patterns That Hold Edge Geometry While Heat Leaves
Getting heat out of a thin edge without pulling it out of shape is less about volume and more about where the fluid lands. A flat fan that wets the wheel face and the shoulder of the bevel at the same time tends to keep the edge steady, because it removes heat from the surrounding mass instead of blasting the apex directly. The edge stays buried in a moving film, so the temperature drops along the grind line rather than jumping from hot to cool in one sharp step.
Split streams aimed at both flanks work well for narrow or delicate profiles. The coolant enters at a shallow angle, follows the bevel for a short distance, and then falls away with the swarf. That shallow contact keeps the mechanical pressure low, which matters when the edge is only a few thousandths thick. A hard jet aimed square at the tip can deflect the very geometry you are trying to hold.
On tall bevels or asymmetric grinds, a low-pressure flood that matches the wheel rotation usually carries heat out more cleanly than a high-velocity stream. The liquid wraps around the steel, absorbs heat, and leaves with the debris instead of slamming the edge sideways. The result is a cooler part and a grind line that does not wander as the metal releases its heat.
The Shrinkage Window Before the First Cutter
The interval between the point where the web leaves its forming or drying stage and the first cutting station is rarely neutral. During this stretch the material continues to release internal stresses, lose moisture, or settle thermally. Treating that distance as fixed often hides subtle changes in width, caliper, and surface tension that arrive at the knife.
Operators who map shrinkage across this window usually measure edge retreat and centerline movement under different line speeds and tensions. A narrow window can force the sheet into the cutter while it is still moving, producing angled edges or uneven sheet lengths. A wider window gives the material room to stabilize, but it also raises questions about space, waste, and curl accumulation.
Adjusting the window is less about choosing a single correct length and more about matching the material's relaxation rate to the downstream tolerance. Small changes in incoming moisture, basis weight, or ambient air movement often show up here before any gauge or vision system flags them.
Matching Water Flow to Line Speed for Uniform Heat Removal
In continuous strip processing, heat removal often suffers because coolant is applied at a fixed rate while the line accelerates or coasts. When the strip moves faster, the same volume of water spreads thinner across each square meter, so local boiling and temperature bands appear. Matching pump output to line speed keeps the water film thickness and contact time consistent.
The practical approach is a speed-following flow curve rather than a fixed valve position. At low threading speeds, flow drops enough to avoid pooling and edge wave cooling; at higher speeds it ramps before the strip reaches the quench zone, so there is no lag when demand spikes. Operators can tune the curve with a simple feed-forward signal plus a small trim based on strip temperature.
Even small mismatches show up as wavy edges or a dull center strip because heat is pulled unevenly across the width. Uniform heat removal depends less on total water volume and more on how evenly that water is delivered per unit of strip passing through. Aligning flow with line speed turns cooling from a rough setting into a repeatable part of the process.
What Steady Cooling Does for Hardness and Cut Faces
A controlled cooling curve does more than bring the temperature down. It lets the structure organize itself before it locks. The result is a hardness that sits deeper and more evenly through the part, rather than a glassy skin over a soft center. You can feel it when a file skates less and bites more predictably near an edge.
Cut faces change as well. With heat leaving at a steady rate, the surface and the interior shrink closer together, so a saw or parting tool exits without tearing out small chips along the line. The cut face comes away smoother, with a settled gray look instead of the rough, oxidized texture that rapid or uneven cooling leaves behind.
It is the pauses and surges in cooling that usually cause trouble. They build stress where the geometry changes or where a cold spot forms. A steady fall through the critical range spreads that contraction across the whole piece, giving the next machining pass a face that stays flat and a hardness that does not wander from corner to corner.
Modular Zones That Absorb Recipe Changes Without Retooling
Most line changes stop being mechanical when the equipment is split into self-contained modules. A dosing unit, a mixing cell, a filling head, or a capping station can each hold its own recipe parameters, so switching from one formula to another no longer means swapping guides, rails, or timing screws. The surrounding zone simply accepts new setpoints and lets the module reconfigure itself within its working envelope.
That self-containment shows up most clearly in short-run production. If a sauce goes from a chunky vegetable base to a smooth emulsion, the pump speed, reverse-flow pulses, and temperature ramp are pushed from the recipe file rather than dialed in by hand. Contact parts that do need to change are mounted on repeatable docking points, which removes the need to realign or retest after every switch.
The quieter benefit is how failures and tweaks stay local. A change in viscosity or particle size may only affect the mixing module, while the filling and sealing modules continue unchanged. Because each zone absorbs its own variation, the line stops being a single brittle chain and starts behaving like a set of independent, recipe-aware cells that can be updated individually.
FAQ
The water flow, spray pattern, and hold time are matched to a specific tread profile and compound. Most of the settings come from short trial runs on the actual product, not from a one-size-fits-all datasheet.
If the surface cools too quickly while the core stays warm, the tread can develop cracks, curl, or shrink unevenly. A controlled gradient keeps the rubber stable through the line and reduces waste at the cutting stage.
Operators can call up stored recipes for each product. The guide rails, nozzle banks, and conveyor speed adjust automatically, so changeover is mostly a matter of selecting the right program and verifying the first piece.
Sensors along the cooling path feed a closed-loop controller. It adjusts water temperature, fan speed, or line speed in small steps, so the tread exits within a narrow temperature band even when plant conditions shift.
The water is recirculated through a filtration skid, and the spray zones shut off when no tread is present. Variable-speed pumps and fans reduce consumption on slower runs or narrow products.
The modular frame allows extra cooling sections to be added without replacing the existing conveyor or controls. That helps when a plant adds a second extrusion line or wants longer residence time for a new compound.
Routine work focuses on spray nozzles, filters, and drive belts. The guards are quick to release and the pump skid is accessible, so cleaning sensors and strainers does not require draining the entire water circuit.
Conclusion
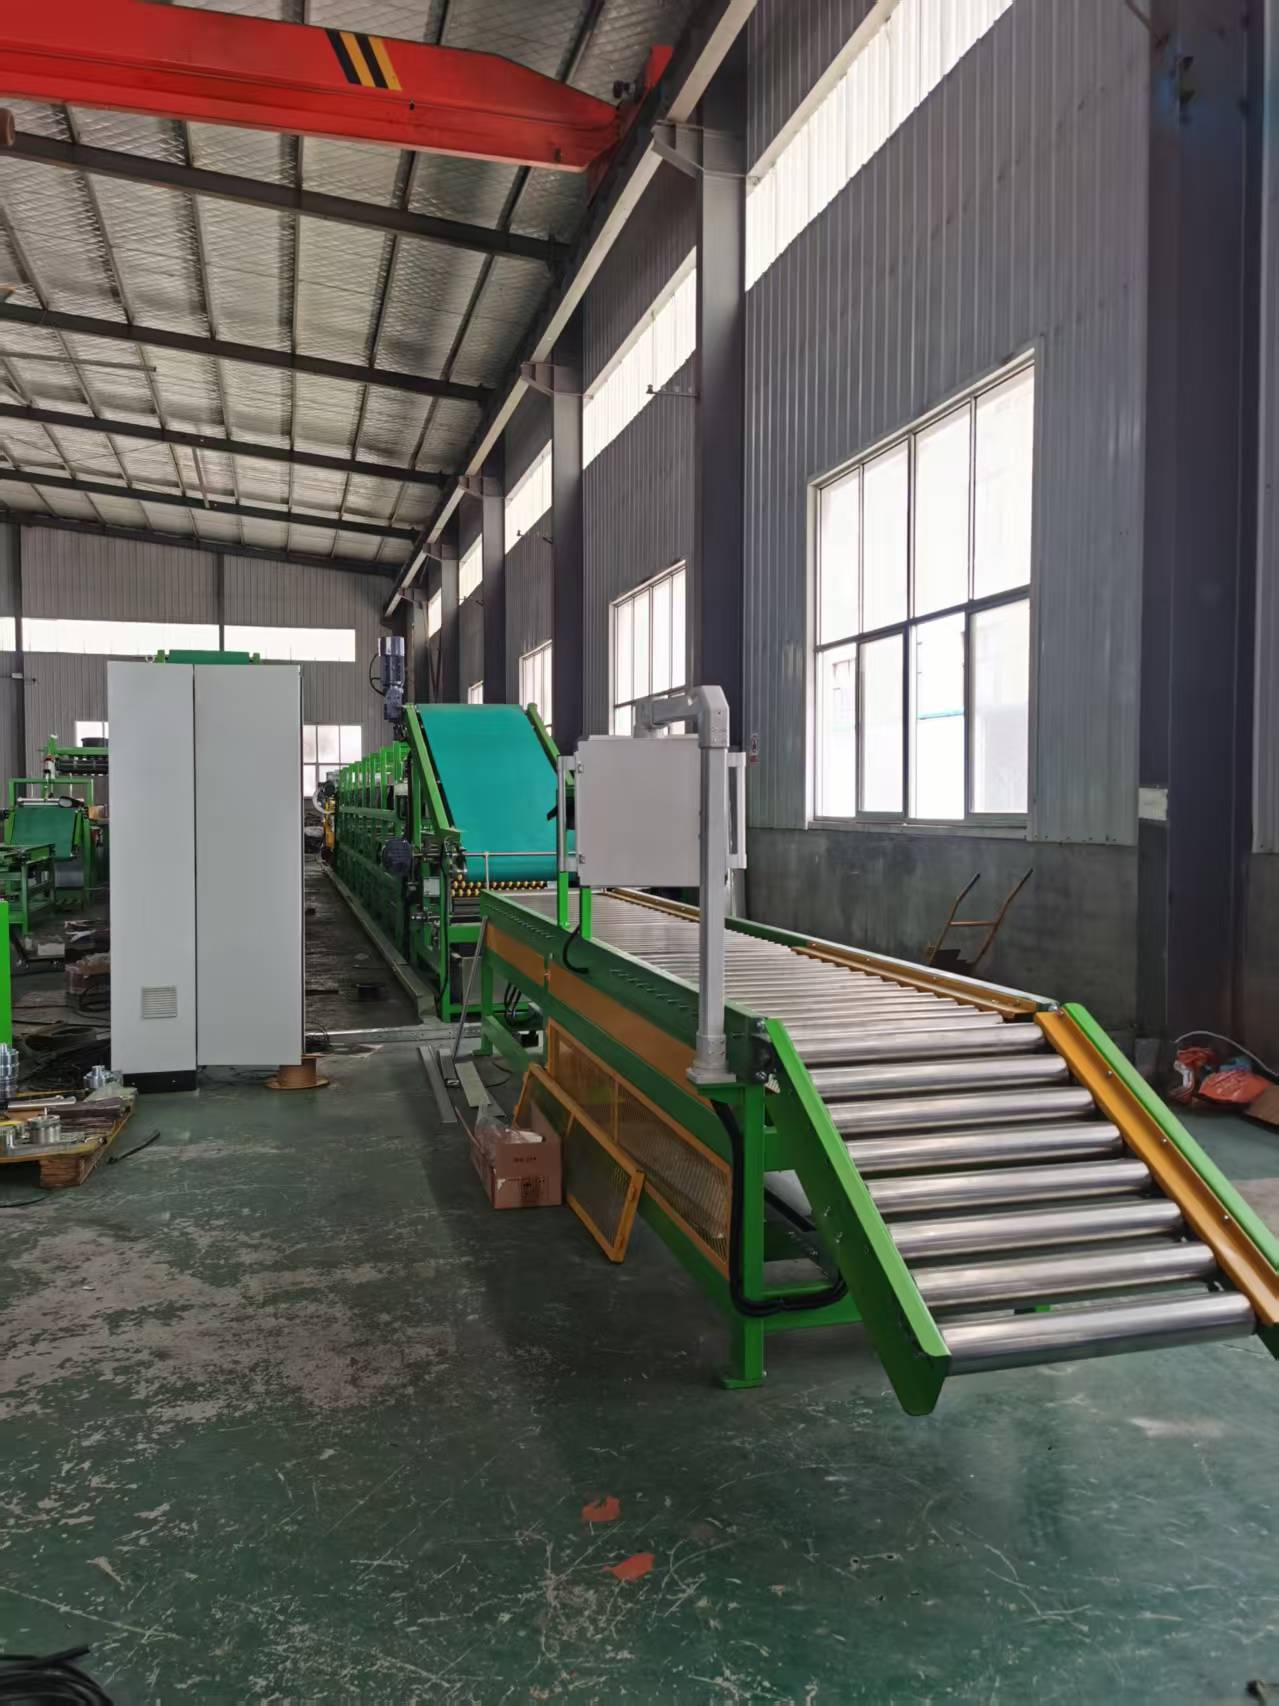
Rather than pushing every tread profile through the same fixed cooling cycle, this line builds the heat-removal path around the actual cross-section and compound. The spray array is positioned so the shoulders and edge radii lose heat without collapsing or rounding, while the center is not drowned in water before the section has stabilized. That matters most in the narrow window before the first cutter. The tread is held in a controlled state until the compound has passed its main shrinkage movement, so the first cut is made on a dimensionally settled strip instead of one still pulling inward.
Water flow is continuously matched to line speed, which keeps the temperature drop even when the line accelerates or slows for a size change. This removes the common pattern of cooler, harder sections followed by warmer spots that cut differently. Downstream, the steadier thermal history shows up as more uniform hardness along the length and cleaner cut faces with less smear or tearing. Because the cooling zones are modular, recipe shifts do not force a mechanical rebuild; settings are changed per zone and the line absorbs the new conditions without retooling. The overall effect is less batch-to-batch drift and a more predictable tread from extruder to cutter.
Contact Us
Contact Person: Lareina
Email: [email protected]
Tel/WhatsApp: +86 17561696737
Website: https://www.auguauto.com/